Mr Whippy Unveils £15 Million Sheffield Doughnut Facility with Advanced Automated Labeling
SHEFFIELD, UK – Iconic dessert brand Mr Whippy is aggressively expanding its footprint in the sweet treats sector, marking a significant strategic shift with the opening of a state-of-the-art 23,355-square-foot manufacturing facility in Sheffield. The £15 million investment signifies the company’s evolution beyond its traditional ice cream roots, with the new site designed to support an ambitious production capacity of approximately 1.5 million doughnuts per week, or roughly 78 million units annually.
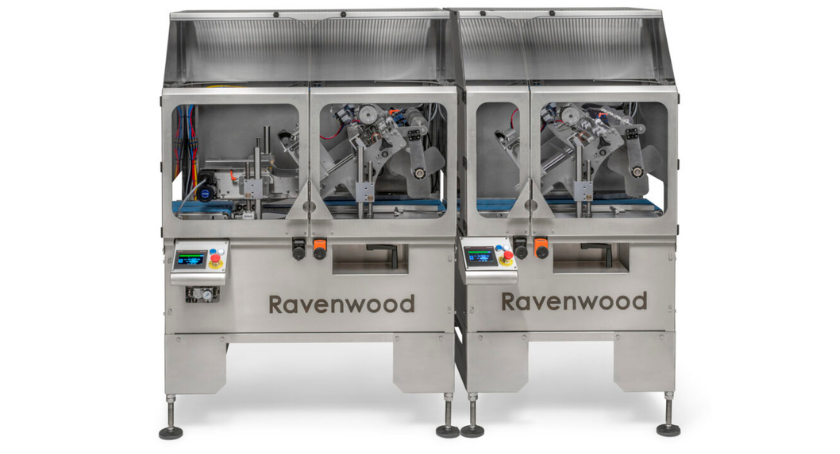
Central to this high-volume operation is the integration of Ravenwood Packaging’s Nobac 5000 Twin Head linerless label applicator. As the facility transitions from baking and cooling to the final packaging stage, the system plays a critical role in maintaining the site’s high-speed throughput. The applicator is configured to apply “D-Wrap” linerless labels across varied product ranges, including two-, four-, and six-pack doughnut configurations.
The choice of the Nobac 5000 Twin Head system was driven by a need for efficiency and minimal downtime. Featuring a dual-head design, the machine accommodates two label rolls simultaneously, which allows for seamless transitions between rolls and significantly reduces the need for operator intervention. This ensures the production line maintains the steady, high-speed flow required to meet the company’s output targets.
“Ravenwood’s linerless technology has been a really important part of our new production facility,” said Michael Jackson, co-founder and CEO of Mr Whippy. “With automation at the heart of the operation, we’ve created a highly streamlined journey from production through to the finished pack, and the Nobac 5000 Twin Head gives us the speed and consistency we need as we scale up.”
Beyond operational speed, the adoption of linerless technology aligns with Mr Whippy’s broader sustainability goals. By eliminating the traditional backing paper associated with conventional pressure-sensitive labels, the company is significantly reducing material waste. The labels, supplied by Ravenwood-approved converter ProPrint Group, provide a clean, retail-ready finish that enhances the brand’s presentation on supermarket shelves.
The Sheffield facility is equipped with the latest advancements in food manufacturing, including modern automated production machinery and energy-efficient CO₂ refrigeration systems. The launch serves as a cornerstone for Mr Whippy’s growth strategy, which includes plans for a second manufacturing site in Manchester dedicated to the production of cakes and cookies.
As Mr Whippy continues to ramp up operations in Sheffield, the company has set a high benchmark for automated food processing. Ravenwood Packaging has confirmed that a comprehensive case study detailing the technical specifics and performance metrics of this installation will be released later this year.
Disclaimer: This content is auto-generated for informational purposes only.
Source: Read Original News